Success Story: How Ultimation Supported a Major Airport Conveyor Retrofit

An engineering and logistics integrator turned to Ultimation, an MCE company, for support on a conveyor system retrofit at a major airport. The project involved upgrading existing baggage-handling equipment to address maintenance and downtime issues while retaining much of the existing infrastructure.

Challenge

The project called for replacing key conveyor components while keeping the existing frames. Any proposed solution needed to meet the facility’s operating requirements.

From the start, the integrator was interested in equipment from Interroll Portec, which Ultimation offers. However, Interroll Portec had not previously been on the airport’s approved vendor list. Once approval was secured, the integrator still needed to demonstrate that the alternative would meet the airport’s technical requirements while offering competitive pricing and lead times.

Complicating matters, the integrator had experienced significant delays in getting a quote from its previous supplier. Moving the project forward required timely pricing, detailed equipment specifications, drawings, and technical documentation to help the integrator evaluate its options and make a recommendation to the airport.

Solution

The integrator worked with the airport to conduct measurements and studies and determine the required conveyor configurations. Ultimation helped the integrator’s engineering team identify equipment that would meet requirements, including speed, load capacity, and the ability to handle different types of baggage, from standard suitcases to boxes, and oversized items such as golf clubs.

Ultimation provided:

  • A detailed quote and itemized equipment list
  • Component drawings and layouts
  • Manufacturer documentation and technical manuals
  • Pricing and lead-time information
  • Direct communication and coordination throughout the quoting process

Ultimation, in partnership with the integrator, chose specialized equipment from Interroll Portec for spiral-belt and straight-belt conveyors. The project used the existing conveyor frames and replaced key internal components, including belts, motors, and other components, to upgrade the equipment.

Ultimation delivered the initial quote in approximately five days, giving the integrator the information it needed to compare the proposed equipment with the previously approved option and move the project forward.

Interroll Portec also supported the project with technical assistance, along with warranty and service support for the equipment.

Outcome

“It was a team effort. The integrator was very pleased with the amount of communication they were getting from our team.” – Janine Nikkel, Inside Sales Rep, Ultimation

The retrofit allowed the facility to upgrade existing equipment rather than replacing the entire conveyor framework, preserving usable infrastructure and reducing the cost and complexity associated with a full system replacement.

The conveyor project’s success came down to more than the equipment itself. Working together with the integrator, Ultimation was able to help them evaluate and sell an alternative solution in a timeline that made sense for their customer.

Communication and responsiveness were also key to success. The previous supplier took several months to provide a quote, delaying a necessary upgrade. Ultimation’s team coordinated the quote process, focusing on both the integrator’s and airport’s needs and providing fast quoting, competitive pricing, strong communication, and transparency throughout the process.

The project moved quickly from the quoting stage in mid-January, with final delivery in the first week of April.

Because of the success of this project, Ultimation is now working with the integrator on a second comparable Phase 2 project for the same facility.
5 Questions to Answer Before Designing an Automated Tire-and-Wheel Transport Conveyor System

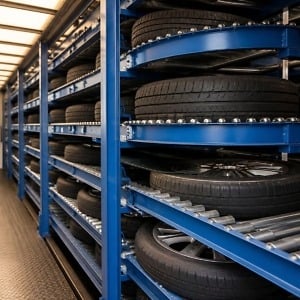
Automated tire-and-wheel conveyor trailers reduce manual handling, maintain sequence from the tire-and-wheel facility through delivery, and keep assemblies moving to the line at the required production rate.

But getting those benefits requires designing the system around the application. Production volume, tire-and-wheel sizes, travel requirements, and the plant itself can all affect what the final system looks like.

We work through those operating requirements with the manufacturer and other partners in the tire-and-wheel program. The process starts by answering five questions about how the system will need to operate.

1. How fast does production need to run?

The expected job rate gives a starting point for determining how much tire-and-wheel capacity needs to move through the system. From there, we consider trailer capacity and how many trailers need to be circulating to support production.

At any given time, one trailer may be loading while another is traveling to the plant, another is unloading, and another is making the return trip. The fleet needs enough capacity across that cycle to keep pace with the assembly line.

Properly sizing the system helps manufacturers maintain the required flow without paying for unnecessary capacity or discovering later that a fleet can’t keep pace.

In one case, our initial calculations indicated that a manufacturer would need more than the two trailers it planned to purchase. As production requirements developed, the manufacturer ultimately added two more.

2. What tire-and-wheel assemblies will the system handle?

Size and weight are important considerations and can have a cascading effect on the system. Larger assemblies take up more physical space, which can reduce the number that fit within a trailer. Additional weight also must be considered when trailers travel on public roads.

Those considerations have become more important as tire-and-wheel assemblies have grown larger, particularly for trucks and other larger vehicles. We look at the full range of assemblies the trailer will need to carry rather than sizing the system around a single tire size or configuration.

That information helps determine a configuration that can accommodate the manufacturer’s product mix while making effective use of available trailer capacity.

3. What does the complete delivery cycle look like?

The number of assemblies a trailer can carry is only part of the capacity picture. We also look at how the trailers will operate between the tire-and-wheel facility and the assembly plant:

  • How far apart are the facilities?
  • How long does loading and unloading take?
  • How quickly does an empty trailer return?
  • How many trailers need to be in circulation at once?

Two plants running at the same production rate could require different trailer fleets. If one tire-and-wheel facility is farther from the assembly plant, each trailer spends more time in transit before it becomes available for the next cycle.

The delivery process also affects how assemblies are handled along the way. An automated system can maintain sequence through transport and unload directly into the plant’s material-handling system, reducing manual transfers between the supplier and the assembly line.

Looking at the complete cycle helps us determine the capacity needed to maintain a consistent supply of assemblies to production.

automated tire and wheel conveyors


4. How will the tire-and-wheel conveyor system fit the existing plant?

We never design a trailer in isolation. Our team looks at how it will dock, connect and operate within the manufacturer’s existing environment.

Details like these are much easier to accommodate during system design than after equipment arrives on site. That makes a review of the dock area and surrounding infrastructure an important part of the process, especially when the system is being added to a facility rather than designed into a new one.

The same applies to the equipment on either side of the trailer. The trailer must work with the loading system at the tire-and-wheel facility and the receiving system at the assembly plant, so we consider those interfaces as part of the application rather than treating the trailer as a standalone piece of equipment.

For example:

  • One facility’s pavement slope required us to account for how the trailer would sit at the dock.
  • An existing structural beam at another plant affected the loading/unloading arrangement.
  • Safety fencing at another application influenced where drivers could connect the trailer.

Those aren’t unusual exceptions, but it’s important to evaluate the actual environment and work with the customer to determine how the system needs to fit within it.

Addressing these conditions during design reduces installation and commissioning problems and creates a smoother interface between transportation and the plant’s existing material-handling system.

5. What might change over the life of the tire-and-wheel equipment?

Automated trailers can remain in operation for decades. During that time, production volumes, vehicle programs, and tire sizes can all change.

That doesn’t mean designing today’s system around every vehicle or tire size a manufacturer might produce someday. But if a new program is already planned, production volumes are expected to change, or larger assemblies are on the roadmap, those requirements are worth discussing before the initial design is finalized.

We have worked with customers to modify existing trailers for new vehicle programs rather than replace equipment that is still mechanically sound. Whether that’s possible depends on how significantly the new requirements differ from the original application.

Considering known changes early can help manufacturers determine where it makes sense to build flexibility into the initial design and potentially extend the useful life of the equipment across multiple programs.

Start With the Application

The right configuration depends on more than how many assemblies need to fit in a trailer. The process starts with understanding how the system needs to operate within the manufacturer’s production and delivery environment.

Taking that approach early helps manufacturers avoid discovering capacity or integration issues later and gives them a system designed to reduce handling, preserve sequence, and keep tire-and-wheel assemblies moving at the rate production requires.

Ultimation, an MCE company, is a turnkey vendor. We help our customers identify the right solution for their operation. This includes:

  • Dock geometry that may need a leveling ramp
  • Safety Restraint Systems
  • Electrical panel to control the trailer operation
  • In-plant conveyors to send or receive the tire/wheel assemblies
  • In-plant tire/wheel buffer system
  • Spare parts supplies to support the trailer lifecycle

Learn more about automated trailers for loading and unloading tire-and-wheel assemblies.

How Choosing the Right Food-Grade Belt Conveyor Boosts Safety and Efficiency

Safe and efficient food handling is top of mind for customers today.

That increased attention puts a spotlight on the need to continuously improve processes, workflows, and tools, while steadily reducing the potential for errors and accidents in food processing and distribution environments.

Choosing the right conveyor setup can help you meet those goals while improving how products move through your facility. Features that simplify cleaning, reduce product damage, and make maintenance easier can help you limit contamination risks while keeping production moving.

Ultimation has added two food-grade belt conveyors to its product lineup, both of which offer stainless steel construction for washdown environments, as well as hygienic designs that make them ideal for food contact applications.

In food-handling environments, conveyor construction also matters because surfaces and components that are easier to access and clean can simplify sanitation routines and help prevent product buildup.

Ultimation Fabric Belt Conveyors provide a smooth, continuous conveying surface in addition to gentle handling of finished goods.

Ultimation Modular Plastic Belt Conveyors are made of plastic modules assembled in an interlocked pattern. Their design makes them both easy to clean and low-maintenance, because damaged modules can be conveniently replaced without having to change out the entire belt.

Both solutions can be adapted to meet specific FDA, USDA, or BEAG sanitary application requirements.

Choosing the Right Food-Grade Conveyor

Keep in mind that there isn’t a single, universal “best” belt conveyor. Homing in on the right conveyor for your facility depends on your needs and requirements. Here’s a short list of questions that can help guide you toward making the right selection.

  • Product: Is the product raw, packaged, frozen, delicate, or abrasive?
  • Sanitation: How often is the conveyor cleaned? What level of washdown is required?
  • Environment: Is the process wet or dry? Is this being used in a low-temperature application such as a freezer, or as an infeed for a high-temperature application such as an oven?
  • Maintenance: How important is minimizing downtime for repairs?
  • Footprint: Are there inclines, declines, or lifters required?
  • Throughput: How quickly does the product need to move across the conveyor line?
  • Controls: Does your operation require an indexing conveyor, continuous run conveyor, or zoned conveyor with Zero-Pressure Accumulation (ZPA) functionality?
  • Integration: Is this conveyor integrating with any other pieces of equipment such as scanners, labelers, or robots?

The answers can narrow the field. Products that require gentle handling and a continuous surface may point toward fabric, while demanding washdown applications or operations where easy belt repair is a priority may favor modular plastic.

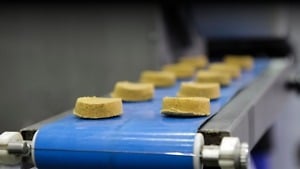
food on food-grade belt conveyor

Fabric vs. Plastic Food-Grade Belts

Fabric belts are the best option for handling small or lightweight items like bakery products, confectionary, or any packaged goods that can benefit from a softer touch and a little extra TLC.

Fabric belts also have the advantage of being more economical than other options. They’re generally considered a good choice for dry processing environments, and are well suited to long product transfers and applications that require a smooth, continuous surface.

Modular plastic belts, on the other hand, are versatile for a wide range of food-production needs, including sanitation, filling, washing, rinsing, inspecting, packaging, and transporting.

They can also be easily reconfigured for different food applications by size, belt type, and other options. They’re generally able to handle heavy product loads.

Modular plastic belts tend to be ideal for facilities that work with raw meat, poultry, and seafood, as well as vegetables and other fresh produce. Applications that require draining or airflow can benefit, too.

Finally, they have the distinction of being maintenance-friendly: the ability to swap in new modules with minimal hassle can really pay off for operations where quick belt repairs translate into reduced downtime. That can be especially valuable in high-throughput operations, where even a relatively short conveyor shutdown can disrupt upstream and downstream processes.

Want to know more? Ultimation’s team of experts can help you identify the best conveyor options for your facility, and configure them for optimal efficiency. Get in touch with us to discuss the possibilities.

Do More With Your Warehouse Space with Powered Flexible Expandable Conveyors

Both time and space are at a premium in warehouse facilities.

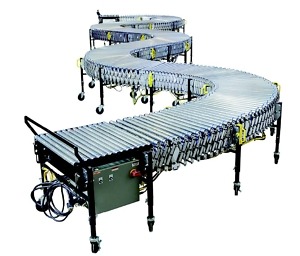
That’s why flexible expandable conveyors are a valuable solution. Like a sofa that pulls out, flexible expandable conveyors expand when you need them and compact when you don’t. This adaptability makes them a cost-effective way to streamline assembly, packing, shipping, and receiving — especially for warehouses that deal with a lot of cross-docking, loading, and unloading.

But as useful as traditional gravity-based flexible expandable conveyors already are, there’s a way to make them even better: power. The powered version of flexible expandable conveyors delivers benefits that can reduce labor while simultaneously boosting efficiency and throughput.

How Adding Power Multiplies FlexibilityULTIMATION Powered Flex Conveyor

Powered flexible expandable conveyors are designed to adapt to your operation in real time.

  • Expands from 3 to 12 feet
  • Bends easily around obstacles and tight spaces
  • Connects seamlessly with additional conveyor units
  • Mounted on casters for easy mobility and positioning

This flexibility allows you to position one end near storage racks and the other at a truck or van for efficient loading and unloading. You can also use them to move products directly from one truck to another.

Because they’re compact when collapsed and quick to deploy, these conveyors can be rolled into place as soon as shipments arrive and then stored away when not in use.

Traditional gravity conveyors still require manual effort and often depend on an incline, making them more labor-intensive. By contrast, powered versions don’t require an incline so they can be deployed anywhere on your floor. Simply roll them into position, plug them in, and let them move product automatically – reducing effort, increasing speed, and improving overall efficiency.

Gravity vs. Powered Conveyors

The advantages of powered flexible expandable conveyors include:

  1. Ease of Use. Powered flexible expandable conveyors feature simple deployment; it only takes one person to set up a conveyor and move it into position. Operating them is similarly easy, with minimal manual handling.
  2. Reduced Labor. That ease of use means that one person can do the same work as three to four people using a gravity conveyor, which multiplies productivity.
  3. Better Ergonomics. By reducing the effort needed, powered flexible expandable conveyors reduce the risk of injury to workers, while also promoting more efficient handling and less chance of damage to products.
  4. Increased Throughput. With more efficient loading and unloading, powered flexible expandable conveyors move more product with less effort, which increases productivity.

A Smaller Footprint

The ability to scale up and scale down in response to changing circumstances has never been more important than it is today. With ongoing labor shortages and rising costs, warehouses are under pressure to do more with fewer workers.

Any innovation that provides warehouses with a way to adapt quickly and efficiently is a boon. Adding power to flexible expandable conveyors means you can get more out of your available warehouse space, without increasing the footprint.

Ready to reduce labor and increase throughput? Contact the team at Ultimation, an MCE company, to speak with a conveyor expert or request a quote.

How VectoRollers™ Boost Efficiency and Reduce Friction to Create a Flexible Flow in the Warehouse

Some ideas are so good for flow, they seem inevitable in retrospect. This is especially true if they apply a little out-of-the-box creative thinking to a long-standing pain point

— like luggage with wheels or self-sealing envelopes.

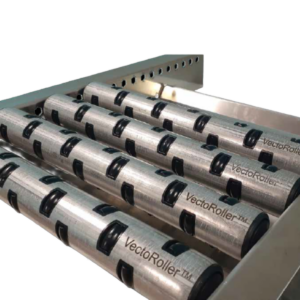
VectoRollers Installed in Gravity Conveyor

For warehouse conveyor systems, VectoRollers™ are a great example of this kind of design breakthrough. It provides an easy, affordable way to minimize the friction that arises when workers need to move products laterally, against the main direction of the conveyor.

By incorporating mini-rollers that run perpendicular to the conveyor’s main direction, VectoRollers™ allow items to easily slide in a lateral direction.

In fact, the VectoRoller™ lateral conveyor design reduces up to 80% the amount of force that’s needed to move packages laterally, compared with regular conveyor systems.

That ergonomic improvement means less strain and fatigue for operators, while allowing packages and products to go with the flow, instead of struggling against it.

The Trouble with Conventional Conveyors for Lateral Movement

Most warehouse conveyors are designed to move product efficiently along a straight line in a single direction. But warehouse reality isn’t always linear. There are times when products need to be intercepted and moved laterally such as at packing stations, quality control checks, and other secondary processes. Items may also need to be repositioned to align with scanners or other equipment.

Traditional conveyor rollers offer significant resistance to sideways movement, making the process harder than it needs to be. Generally, this means extra effort is required at pick, merge, and sorting points.

For warehouse workers, trying to move product against the main flow can be like swimming against a current. Lifting, pushing, or pulling products to move them laterally causes strain, fatigue, and stress. In addition to causing a slowdown in momentum and creating a drag on productivity, this can raise the risk of damage to products and injury to employees.

The impact is magnified given the speed at which modern warehouses need to move, due to higher volumes, mounting competition, and increased demands from customers — as well as the challenges of recruiting and retaining qualified team members in times of labor scarcity.

Why Some Lateral Conveyor Solutions Fall Short

In the past, warehouses have commonly used one of two different approaches for moving products in a lateral direction. But both methods come with drawbacks.

1. A ball transfer table (or ball transfer unit system) is a material-handling surface made up of many small, load-bearing balls that are mounted inside larger housings. Each unit contains a large main ball that sits on smaller support bearings, which allow it to rotate freely in any direction.

The catch is that this approach works best with rigid, flat-bottomed products. It’s less effective for packages with soft undersides or uneven surfaces, and very small items can be problematic as well.

Ball transfer tables are also vulnerable to dirt and debris, which can adversely affect performance. And it’s less than ideal when you need a controlled directional flow, since it allows items to move in any direction rather than just one specified counter-direction.

2. A pop-up transfer station consists of a powered conveyor mechanism that’s used to move products from one conveyor line to another, either at a right angle or moving in a different direction. These are often used in automated sorting systems, for diverting products to different lines, or when changing directions in high-throughput systems.

The main issue here is cost, because pop-up transfer stations tend to be expensive. And they still don’t provide the degree of ease and flexibility that’s needed to boost productivity and keep up with demand.

Rugged and Ready to Roll: VectoRollers™ Are Retrofit-Friendly and Built to Last

That’s where VectoRollers™ come in. Their perpendicular mini-rollers provide ease of lateral movement by rotating in the direction of travel, minimizing the resistance between the roller contact surface and the package in motion. And their proprietary wheels can be mounted at rates of up to two wheels per inch of effective tube width, to optimize the reduction in friction for a specific application.

Watch now: VectoRoller™ in Action


But despite the revolutionary benefits they deliver, VectoRollers™ don’t require a radical investment. In fact, they’re designed for easy, retrofit-ready installation, with no structural changes to conveyors required.

This makes them:

  • Cost-effective and budget-friendly. You can get all the benefits of VectoRollers™ without the need to install new conveyor equipment. And they’re scalable, too. Just swap them in as a replacement for existing rollers, whether gravity-based or powered, upgrading on your own timetable.
  • Easy to maintain. VectoRollers™ are customizable to include different groove profiles, which allows VectoRollers™ to play well with existing systems. Configurations are available for gravity, O-ring, poly-rib, and belt-driven live roller (BDLR) applications. And their 7/16” spring-retained hex axle optimizes ease of installation.
  • Built to be strong. They have a triple-layer coating that provides corrosion resistance, as well as superior cosmetics. And VectoRollers™ feature precision bearings for increased load capacity, speed, and durability, which maximizes their longevity in high-performance applications and settings.

Ultimation’s team of experts is ready to help you take advantage of the latest innovations that can boost warehouse efficiency and productivity. Get in touch to discuss the possibilities.

Subscribe to the Ultimation Newsletter